
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
iTechGuides is reader-supported. When you buy through links on our site, we may earn an affiliate commission. As an Amazon Associate I earn from qualifying purchases. Learn more
Choose the process that can make the part you actually need. Desktop Metal systems are for projects that require metal and can accommodate specialized printing and post-processing. FDM is a fit for thermoplastic parts made by extrusion; resin printing is a fit when a photopolymer process and its material options suit the design. There is no universal winner: compare the specific machine, material, geometry, production quantity, finishing needs and total workflow.
What does “Desktop Metal 3D printing” mean?
It does not refer to one process. Desktop Metal’s metal lineup includes binder jetting and bound metal deposition (BMD). Both begin with metal feedstock and require post-processing to produce the finished metal part, but they form the printed shape differently. “Desktop” in the company’s name should not be taken to mean that every system is a small consumer printer or uses the same process as an ordinary plastic machine.
Binder jetting: Shop System and X-Series
In binder jetting, a printhead deposits liquid binder selectively onto layers of metal powder. The resulting printed part is not yet the finished metal component: it must be handled and processed, including depowdering and furnace sintering. Desktop Metal describes the Shop System workflow as printing, depowdering and sintering. Its X-Series is also a binder-jet family and includes systems for metals or ceramics; specifications differ by model.
Recommended Free Tools
Bound metal deposition: Studio System 2
Studio System 2 uses BMD. It extrudes bound metal rods, a motion that Desktop Metal says is similar to FDM, but the feedstock is metal powder held in binder, not ordinary plastic filament. The printed “green” part then goes into a furnace, where binder is removed and metal particles sinter. Desktop Metal describes the system as office-oriented, but it remains a specialized metal workflow rather than a standard plastic desktop printer.
#1 Best Overall

- One-Click Automatic Printing: Experience hassle-free 3D printing with the Adventurer 5M Series. Enjoy automatic bed leveling for flawless first layers, ensuring consistent adhesion and saving time with no manual adjustments required.
- 12X Ultra Fast Printing: Featuring a CoreXY structure with 600mm/s travel speed and 20000mm/s² acceleration, the AD5M maximizes efficiency, reduces production cycles, and ensures high precision, making it ideal for rapid prototyping and mass production.
- Smart and Efficient Design: Quick 3-second nozzle changes, a high-flow 32mm³/s nozzle, and fast 35-second warm-up to 200°C deliver stable high-speed printing. Its dual-sided PEI platform and versatile options provide easy removal and adaptability for various creative projects.
- Superior Print Quality & Adaptability: Combines a 280°C direct drive extruder with dual-fan cooling and vibration compensation. Includes a standard 0.4mm nozzle and accepts optional sizes from 0.25mm to 0.8mm to fit various printing needs.
- Real-Time App Monitoring: Monitor print progress, adjust settings, and receive instant status alerts remotely with the Flash Studio. Smart mobile control ensures a seamless, effortless printing experience anytime, anywhere.
Desktop Metal states that Studio System 2 parts can “densify up to 98%.” That is a vendor claim, not an independently verified result for every part or material. The finished outcome depends on the specified material and process, so do not treat that figure as a guarantee for an arbitrary design.
FDM and resin are different material routes
FDM builds plastic parts by extruding thermoplastic material. Resin/SLA systems use photopolymer resin and light-based curing. The Formlabs Form 4 is one current US-market example of a resin printer with a materials and post-processing ecosystem; it is not representative of every resin machine. These processes do not directly produce the same material outcome as a sintered metal system.
Which process is right for my project?
Start by writing down the part’s required material and function. If the design must be metal, ordinary plastic FDM or resin printing is not a substitute. If a suitable plastic part meets the need, weigh the plastic workflows against each other rather than assuming that metal is automatically better.
Rank #2
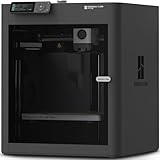
- Up to 16 Colors: Bring your designs to life with vibrant multi-color/multi-material printing capabilities, perfect for showcasing your creativity. Note: Connecting Bambu Lab AMS is required.
- 500mm/s and 20000 mm/s² Acceleration True High Speed: Don't wait around for your masterpieces. Lightning-fast printing speed lets you focus on creating, not waiting.
- Enclosed Design: Fully enclosed body improves print performance for advanced filaments. Automatic Bed Leveling: Say hello to high-quality, successful prints. Auto bed leveling makes 3D printing such an easy thing.
- Set Up in 15 Minutes: Spend more time printing and less time setting up. User-friendly design ensures a hassle-free assembly experience for all skill levels.
- Supported Filament: Ideal: PLA, PETG, TPU, PVA, PET ABS, ASA; Capable : PA, PC; Not Recommended: Carbon/Glass Fiber Reinforced Polymer.
| Project requirement | Metal printing | FDM | Resin/SLA |
|---|---|---|---|
| Part must be metal | Relevant option; Desktop Metal examples use binder jetting or BMD and require post-processing. | Not an equivalent metal output; the comparison here is plastic extrusion. | Not an equivalent metal output; the process uses photopolymer resin. |
| Part can be plastic | May add a metal workflow that the project does not need; assess the actual function and economics. | Consider when thermoplastic material and extrusion fit the part. | Consider when a photopolymer workflow and its material options fit the part. |
| Geometry or tooling benefits from additive design | Desktop Metal describes complex tooling and conformal cooling as applications; these are vendor examples, not a guarantee for every design. | Suitability depends on the chosen printer, material and geometry; the cited sources do not establish a universal comparison. | Suitability depends on the chosen printer, material and geometry; the cited sources do not establish a universal comparison. |
| Production quantity or batch size matters | Compare the particular system’s build envelope, batch plan and throughput; specifications vary across models. | Check the specific machine’s build capacity and production plan. | Check the specific machine’s build capacity and production plan. |
| Post-processing and operations are constrained | Plan for system-specific steps such as powder handling, depowdering, debinding or furnace sintering. | Use the selected printer and material’s instructions to determine handling and finishing needs. | Use the selected printer and material’s instructions to determine resin handling and post-processing needs. |
The table is a screening tool, not a material-property ranking. The available manufacturer sources support the broad distinction between metal, thermoplastic and photopolymer routes, but they do not provide a neutral, universal ranking of strength, stiffness, corrosion resistance, temperature behavior or machinability across all materials. Compare the data for the exact material and process you plan to use.
What should I compare before choosing?
A technology label is only the beginning. Make the decision against your part requirements and the complete production route, not the printer’s headline description.
1. Required material and part function
List what the finished part needs to do: carry load, remain stiff, resist corrosion, tolerate a particular temperature, or be machinable afterward. Desktop Metal cites stiffness, strength, corrosion resistance and machinability as reasons metal may be relevant for its intended applications. Those are use-case considerations, not proof that every metal print will outperform every plastic part. Confirm the chosen material’s specifications and qualify the design for its actual use.
Rank #3

- Vivid Multi-Color Printing: Bring your creations to life with vibrant, multi-color prints. This printer supports up to 4 colors simultaneously, giving you endless creative possibilities.
- 1-Click Auto Leveling: Enjoy smooth, uninterrupted prints with the advanced 1-Click Auto Leveling feature that automatically calibrates your print bed for optimal results every time.
- Ultra-Fast 12X Printing Speed: The AD5X features a Core XY structure with speeds up to 600mm/s and acceleration of 20,000mm/s². Its stable design boosts both efficiency and print quality, making it ideal for rapid prototyping and batch production.
- Exceptional Print Quality: The AD5X delivers outstanding print results with its advanced dual-channel cooling fan, vibration compensation system, and 300°C direct-drive extruder.
- Versatile Nozzle Options: The AD5X supports four nozzle sizes (0.25mm to 0.8mm) for full creative control. The 0.4mm nozzle comes pre-installed for versatile, everyday printing. For specialized tasks, optionally upgrade to the ultra-fine 0.25mm nozzle for miniature details, or to the 0.6mm/0.8mm nozzles to slash print time on large, sturdy models.
2. Geometry and design intent
Ask whether the design benefits from additive geometry, and whether it can be produced and finished with the selected process. Desktop Metal highlights complex tooling and conformal cooling as metal-printing use cases. That does not establish that printing is the best method for every tool or cooling channel; assess the part’s geometry, production needs and finishing route.
The Tool Desk
Outbyte Driver Updater FREEScan for outdated or missing drivers - takes under a minuteDriver Scan →Outbyte PC Repair FREERepair Windows errors before they cause bigger problemsFix Now →3. Quantity, build envelope and throughput
Estimate the number of parts and when they are needed. Then compare the actual machine’s usable build capacity, batch arrangement and expected throughput. A published build size is not the same thing as a production-rate guarantee, and a specification for one model cannot be applied to a whole product family.
4. Full workflow and operational burden
Map every step from feedstock to accepted part. Metal systems can involve powder handling, depowdering, debinding and furnace sintering, depending on the process. Resin systems have their own material handling and post-processing requirements; consult the instructions for the selected printer and material. Include labor, facilities, equipment and any step that will be outsourced—not just the print itself.
Rank #4

- 600mm/s Speed & CoreXY Structure — Powered by an all-metal CoreXY frame and 20,000mm/s² acceleration, Adventurer 5M Pro reaches speeds up to 600mm/s. Integrated vibration compensation algorithms eliminate ghosting and ringing for smooth, high-precision surface finishes.
- 3-Second Quick-Swap Nozzle & Auto Leveling — Features a tool-free, quick-release nozzle mechanism for effortless 3-second replacements across multiple sizes (0.25/0.4/0.6/0.8mm). One-click full auto-leveling ensures precise bed calibration and a perfect first layer every time.
- Dual Filtration System & Quiet Enclosure — Built with an integrated dual filtration system and a fully enclosed chamber to ensure a clean printing environment and thermal stability. Powered by low-noise motion control, it operates quietly under 50dB for seamless home, office, or classroom use.
- 280°C High-Temp Extruder & Broad Material Compatibility — With a 280°C max nozzle temperature and a 110°C heated bed, it reliably prints engineering materials like ABS, ASA, and PETG-CF, as well as standard PLA and PETG.
- Smart Camera & Mobile Control — Features a built-in camera for real-time monitoring and time-lapse video creation. Monitor progress, adjust settings, and receive instant status alerts via Flash Studio. Integrated with filament detection, power loss recovery, and a 4.3-inch touchscreen for effortless operation.
5. Total project cost
Compare equipment, materials, labor, facilities, post-processing and outsourced work for the same part and production plan. The reviewed manufacturer pages do not establish a neutral, current, like-for-like cost comparison among Desktop Metal, FDM and resin. Desktop Metal’s reviewed product pages do not publish standard purchase prices; they provide order or contact paths. Obtain current quotes for the exact equipment and workflow before making a financial comparison.
What do the Desktop Metal examples tell me?
The published figures below describe particular products, not all metal printers. Desktop Metal’s product pages were checked in 2026; treat their specifications and performance statements as vendor-published information.
| Example | Process and workflow | Published specification or scope | What not to infer |
|---|---|---|---|
| Shop System | Binder jetting; product page describes a printer, powder station/depowdering and a sintering furnace. | One listed build size is 350 × 220 × 200 mm, with smaller height options also published. | This is not a universal build size for Desktop Metal or metal printers generally. The reviewed page does not publish a standard purchase price. |
| Studio System 2 | BMD; bound metal rods are extruded, then the green part goes through furnace processing. | Published build area: 30 × 20 × 20 cm. Desktop Metal states densification up to 98% after sintering. | The densification figure is a vendor statement, not an assurance that every part reaches that result. |
| X-Series | Binder jetting family for metals or ceramics. | The family page lists model-level envelopes and maximum build rates. | There is no single build envelope or maximum rate that can be generalized across the family. |
| Stratasys FDM catalog | Official US and Canada FDM printer category. | Useful as a reference for the FDM product class. | It is not a direct cost or performance comparison with a Desktop Metal system. |
| Formlabs Form 4 | Resin/SLA product example for the US market. | The product page presents a resin printer and links it to materials and post-processing. | It is one product example, not a proxy for every resin printer. |
Can a desktop 3D printer print metal?
Some metal systems are designed for office or smaller-footprint settings, but that does not make them equivalent to ordinary consumer FDM or resin printers. Studio System 2, for example, uses a bound-metal feedstock and requires furnace processing. Binder-jet systems such as the Shop System also need a dedicated powder and sintering workflow. The question is not just whether a machine can print a shape: it is whether the complete system can make the required qualified part within your operating constraints.
Best Value

- High-Speed Precision: Experience unparalleled speed and precision with the Bambu Lab A1 3D Printer. With an impressive acceleration of 10,000 mm/s², the A1 delivers blazing-fast printing while maintaining exceptional accuracy and detail in your prints.
- Multi-Color Printing with AMS lite: Unlock your creativity with vibrant and multi-colored 3D prints. The Bambu Lab A1 3D printers make multi-color printing accessible and reliable for everyone, bringing your designs to life in stunning detail. Note: AMS lite required, get A1 Combo or buy AMS lite seperately.
- Full-Auto Calibration: Say goodbye to manual calibration hassles. The A1 3D printer takes care of all the calibration processes automatically, ensuring optimal performance for every print. Enjoy a seamless printing experience with precise Z-offset, bed-leveling, and more.
- Active Flow Rate Compensation: Achieve consistently smooth prints with active flow rate compensation. The algorithm actively compensates the flow rate according to the readings to extrude with accuracy, ensuring flawless prints.
- Easy and Quiet 3D Printing: Experience effortless printing with the Bambu Lab A1 FDM 3D printer. Its user-friendly interface and simplified touchscreen make it easy to use. The 1-Clip quick swap nozzle ensures convenient maintenance and provides versatile printing options. Enjoy a quiet printing environment with active motor noise canceling, allowing you to focus on your work while the A1 FDM 3D printer brings your ideas to life
How should I make the decision step by step?
- Define the part. Record the required material, function, geometry, finish, quantity and acceptance criteria. Identify which requirements are essential and which are preferences.
- Eliminate material mismatches. If the finished component must be metal, do not treat plastic FDM or resin as equivalent. If plastic is acceptable, keep both plastic processes in consideration.
- Shortlist a specific machine and material. Compare real models, not broad labels. For metal, distinguish BMD from binder jetting; for plastic, identify the exact thermoplastic or photopolymer workflow.
- Map the post-processing chain. Write down each required step after printing, the equipment and handling it needs, and who will perform it. Include outsourced operations in the plan.
- Check capacity against the job. Verify the model’s build envelope and how the intended batch fits. Use family-level maximums only when the specific model and conditions match.
- Compare total cost and schedule. Request current quotes where prices are not public and cost the entire route, including labor, facilities, materials and finishing. Do not assume a vendor’s general speed or cost claims establish a head-to-head advantage.
- Validate with the actual part. Review the selected material and process data, then establish whether a sample or qualification run is needed for the part’s use. Application examples from a manufacturer do not replace part-specific validation.
What are the common selection mistakes?
- Calling all Desktop Metal systems the same process. The lineup includes both binder jetting and BMD, with different feedstocks and workflows.
- Assuming “similar to FDM” means the same output. Studio System 2’s extrusion motion is described as similar to FDM, but its feedstock is bound metal and it requires sintering.
- Expecting ordinary FDM or resin printing to produce equivalent metal parts. The compared plastic processes use thermoplastic or photopolymer materials, not a sintered metal feedstock.
- Choosing by a headline specification alone. Build size, build rate and workflow are model-specific; they do not by themselves establish part quality, cost or production fit.
- Taking application or economic claims as independent comparisons. Desktop Metal’s application examples and vendor claims are not neutral, like-for-like results across technologies.
- Comparing printer prices instead of project costs. Equipment is only one part of a metal, FDM or resin workflow; account for materials, labor, facilities and post-processing.
Which process is the practical choice?
Choose Desktop Metal when the project’s required outcome is a metal part and the selected system’s geometry, capacity and post-processing chain fit the job. Choose FDM when thermoplastic material and extrusion are sufficient. Choose resin when a photopolymer workflow and its material options suit the part. If the material requirement is not yet clear, resolve that first; technology comparisons made before that decision can send the project toward an unnecessary workflow.
For further product-specific details, consult the manufacturers’ official pages: Desktop Metal’s “Metal Binder Jetting — How Does it Work?” and “Introduction to the Binder Jetting Process,” “Shop System,” “Studio System 2,” “Metal 3D Printers,” “Key Applications for Metal 3D Printing on the Studio System,” and *The Ultimate Guide to Laser-Free Metal 3D Printing with Binder Jetting Technology* (2023); Stratasys’s US FDM printer catalog; and Formlabs’s US Form 4 product page. Product claims and specifications should be read in the context of the named machine and material.
Frequently Asked Questions
Is metal 3D printing the same as metal CNC machining?
No. The processes make parts differently, and the sources cited here do not establish which is better for any particular design. Compare the geometry, material requirements, production quantity and finishing route before selecting a manufacturing method.
Free tools Windows power users keep installed
One-click scans. No signup required.
Can I use the same design file for FDM, resin and metal printing?
A shared digital model does not ensure that a design is suitable for every process. Each route has its own feedstock and processing steps, so check the selected machine and material requirements and validate the part for its intended use.
Does Desktop Metal make ceramic printers too?
Desktop Metal’s X-Series family page includes systems for metals or ceramics. The family’s model-level specifications differ, so check the specific system rather than assuming every X-Series machine supports the same material or capacity.
Is Studio System 2 suitable for a home workshop?
The vendor describes it as office-oriented, but that label alone does not establish that it fits a home setting. Its workflow includes furnace processing, so assess the complete system, facilities and operating requirements before considering a location.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

