
Free tools Windows power users keep installed
One-click scans. No signup required.
Powder coating usually leaves a metal part conductive inside, but changes the electrical behavior of its coated surfaces and joints. The cured polymer film is typically a high-resistance barrier: it can block contact to the metal, interrupt grounding or EMI bonds, and provide insulation when a suitable product is specified and tested. The outcome depends on the coating formulation, thickness, cure, geometry, and service environment.
What changes—and what does not
Powder coating applies charged resin-and-pigment particles to a grounded metal workpiece, then melts and cures them into a film. Grounding the part during application helps attract powder; it does not make the finished film conductive. ASTM describes the application process in D7803.
For ordinary thermoset coatings, the steel, aluminum, copper, or zinc beneath the film generally retains its bulk conductivity. What changes is the electrical path available at the surface: a probe, fastener, terminal, gasket, or adjoining panel meets coating rather than bare metal. Consequently, surface resistance, contact resistance, and insulation behavior can change sharply even when current can still flow freely within the metal.
- Bulk conductivity describes current flow through the metal itself.
- Surface resistance describes current flow across the coating surface.
- Volume resistivity describes resistance through the coating material.
- Contact resistance describes resistance at a connection or interface.
- Insulation resistance describes leakage between electrically separated conductors.
- Ground-bond resistance describes continuity through a protective bonding path.
These values answer different questions and are not interchangeable. Exceptional process heat, substrate oxidation or damage, and specialty formulations can alter the result, so bulk conductivity should not be assumed unchanged where the process or material is unusual.
Do these 3 things before closing this tab:
1Scan for outdated or missing drivers - takes under a minute2Clear out junk files and repair common Windows errors3Fix the driver behind crashes, sound loss and screen glitches#1 Best Overall

- Versatile Powder Coating: This system allows you to powder coat a wide range of materials including metal, wood, plastic, and more with its dual voltage (15KV and 25KV) capabilities.
- Efficient Coating: The powerful electrostatic charge ensures efficient and even powder coating, minimizing waste and maximizing coverage.
- User-Friendly Design: The clear bottle design allows you to easily monitor powder levels, while the ergonomic gun handle ensures comfortable operation.
- Compact and Portable: With its compact size and lightweight construction, this powder coating machine is easy to transport and store.
- Reliable Performance: Constructed with high-quality materials, this powder coating system delivers consistent and reliable performance for your various coating projects.
Electrical effects of the coating
Surface resistance and electrostatic behavior
Most decorative powder coatings present a high-resistance surface. Some specialty products are conductive or static-dissipative, but the labels are test-defined. IGP describes ESD-related resistance classes, including conductive values below about 104 Ω, intermediate dissipative behavior in ranges that depend on the classification scheme, and insulating values above 1011 Ω. Those figures only make sense with the relevant method, electrode arrangement, conditioning, and measurement conditions; see IGP’s technical information and its measurement guidance.
An ESD-dissipative surface controls charge bleed-off. It is not a protective-earth bond, a guarantee of EMI shielding, or a high-voltage insulation system. A coating may conduct laterally across its surface yet still fail to provide a reliable low-impedance connection to the metal underneath.
Contact and insulation resistance
A film between two contacting parts can make resistance high or unpredictable. This commonly affects grounding lugs, hinges, enclosure seams, mounting brackets, busbar supports, cable glands, fasteners, and test points. Thickness, hardness, compression, oxide layers, hardware geometry, and whether a fastener truly breaks through the film all matter.
Rank #2

- The PCS-250 Makes Powder Easy To Apply and Provides Extremely Durable Finish. Economical - Quick Color Changes - Coat and Cure In Under An Hour
- Low 15,000-Volt Setting and High 25,000-Volt Setting For Multi-Coat Coverage Over Larger Areas. Versatility with two settings for improved coverage
- The Hotcoat Benchtop Oven Heats Up Fast With Upper and Lower Heating Elements with a Air Circulation Fan Allow Optimum Control of Heat Distribution
- The Powder Coating Booth Captures Over 95% of Powder Overspray and is a Compact Size and Easy to Assemble
- Uses Your Standard 20 Inch Box Fan. Perfect For Powder Coating in a Garage or Small Shop
Conversely, a coating can isolate a conductor from a nearby metal part. That is useful for busbars, motor components, battery assemblies, and other electrical hardware, but ordinary decorative powder is not automatically a qualified dielectric. Specify a product and process with data for the needed thickness, cure, temperature, humidity, and geometry.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
Dielectric strength and breakdown
Dielectric strength is the electric field a material withstands before breakdown, commonly expressed in kV/mm. It is different from insulation resistance. For an ideal, uniform film, a rough estimate is breakdown voltage ≈ dielectric strength × thickness; it is not a safe working-voltage rating.
Product data illustrate why values must be tied to a specific formulation and test. AkzoNobel Resicoat EL datasheets give example dielectric-strength values above 45 kV/mm or in a 30–45 kV/mm range, depending on product, alongside product-specific thickness and test information: HZG15R, HLF59R, and EL201 HFF09QF. These are not universal allowances for powder coating. Pinholes, thin edges, voids, contamination, poor cure, cracks, moisture, and concentrated electric fields can cause real parts to break down earlier than a uniform coupon suggests.
Rank #3

- 𝐏𝐎𝐖𝐃𝐄𝐑 𝐂𝐎𝐀𝐓𝐈𝐍𝐆 𝐒𝐘𝐒𝐓𝐄𝐌: 𝐄𝐞𝐚𝐬𝐭𝐰𝐨𝐨𝐝'𝐬 𝐏𝐂𝐒-𝟐𝟓𝟎 dual-voltage powder coating system is a breakthrough refinishing system for the home hobbyist providing professional performance at a fraction of the cost of industrial equipment. The cured finish resists most chemicals, fuels, acids, thinners, brake fluid, UV light, and is much more durable than liquid coatings (up to ten times).
- 𝐁𝐄𝐒𝐓 𝐔𝐒𝐄: Powder coating is a very popular type of finishing for steel and other metallic products. It protects the surface from scratches, chipping and corrosion. Additionally, it is the most durable finish available today because it offers a high scratch resistance as well as weatherproofing to prevent corrosion.
- 𝐄𝐀𝐒𝐓𝐖𝐎𝐎𝐃 𝐐𝐔𝐀𝐋𝐈𝐓𝐘: Eastwood offers solutions which combines our 4,000+ unique products with the know-how to “𝐃𝐨 𝐓𝐡𝐞 𝐉𝐨𝐛 𝐑𝐢𝐠𝐡𝐭”. With an In-house product design, development and testing and a strong track record of high-quality, innovative products. Used and trusted by top builders to beginners and also provides a Lifetime Tech Support.
- 𝐖𝐇𝐀𝐓'𝐒 𝐈𝐍 𝐓𝐇𝐄 𝐏𝐀𝐂𝐊𝐀𝐆𝐄: PCS-250 Dual-Voltage HotCoat Powder Coating Gun, dual-voltage power supply, activation switch, ground clamp and cable, and an empty 8-oz. clear bottle.
- 𝐖𝐀𝐑𝐑𝐀𝐍𝐓𝐘: Comes with a 1-year limited warranty and 90-day return.
Capacitance, AC behavior, and heat
A coating is also a dielectric layer between the metal and nearby conductors. Electrical-insulation powder datasheets specify relative permittivity values around 2–4 for some products, with dissipation-factor results over stated frequency ranges. This can change capacitance, coupling, leakage paths, and high-frequency impedance at joints. The effect may be negligible on an ordinary low-frequency structure but deserves analysis and testing in busbars, sensors, high-voltage equipment, RF enclosures, and precision capacitive systems.
Powder coating is much less thermally conductive than its metal substrate. Example insulation-product datasheets report coating thermal conductivity around 0.16–0.50 W/(m·K), depending on product. A thin decorative film on a large enclosure may have little system-level effect; a thick dielectric layer on a high-current busbar can impede heat transfer and affect temperature rise or current capacity. Evaluate the actual assembly rather than extrapolating a material value directly to whole-part performance.
Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchWindows Errors? Fix Them Before They Spread
Repair common Windows errors and clear accumulated junk for a smoother, more stable PC - no reinstall needed.Free scan · no reinstallGrounding, bonding, and EMI shielding
A coated surface is normally not a dependable electrical contact. Plan grounding pads, bonding points, test locations, hinges, removable-panel seams, and EMI contact lands before coating. Common approaches include masking the contact area, clearing coating after cure, using a designed penetrating fastener, adding a bonding jumper or conductive gasket, or installing a dedicated grounding stud after coating.
Rank #4

- Powder Coating Gun Operates on standard 120v / 60Hz household current
- Versatility with two settings for improved coverage - Low 15,000-volt setting and High 25,000-volt setting for multi-coat coverage over larger areas
- Clear bottle allows you to see powder color, level and fluidizing action and Larger internal passages for improved powder flow
- Oven is Ideal for Small to Mid-Size Powder Coating Projects
- Oven Heats Up Fast With Upper and Lower Heating Elements and Air Circulation Fan Allow Optimum Control of Heat Distribution
- Masking can create a clean, predictable bare-metal land, but requires accurate drawings and process control; masking can shift or leave ridges.
- Post-coat removal can accommodate late changes, but may leave residue, damage adjacent coating, reduce repeatability, or expose corrosion-prone metal.
- Serrated washers and penetrating screws may establish contact, but their success depends on coating thickness and hardness, torque, oxide or pretreatment layers, vibration, corrosion, and repeated assembly.
- Bonding jumpers and conductive gaskets can preserve continuity across moving or removable joints when properly selected and validated.
Test the completed joint rather than assuming that a screw has pierced the film. Aluminum and copper can form resistive oxide layers even at an apparently bare contact; surface preparation, contact pressure, plating, hardware, and corrosion control still matter.
The metal wall of a coated enclosure may continue to shield effectively, while coating trapped between a door, cover, seam, hinge, or fastener can disrupt low-impedance continuity and degrade EMI performance. A standard insulating powder is not an EMI-shielding coating. Use conductive contact lands or appropriate gaskets and validate shielding at the assembled seams. Product categories for insulation and ESD/conductivity are treated separately by TIGER Drylac.
The Powder Coating Institute gives 1 MΩ or less as a maximum resistance-to-ground figure in its cited transfer-efficiency process guidance, where powder buildup on hangers and contact points can degrade application grounding. That production-process figure is not a protective-earth or finished-equipment bonding requirement; use the applicable product and jurisdictional standard for those. See the Institute FAQ.
Best Value
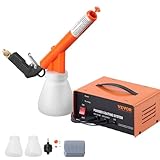
- Strong Electrostatic Adhesion: VEVOR powder coating system boasts a 50KV electrostatic output, ensuring superior adhesion of the coating to surfaces. The resulting coating exhibits exceptional resistance to cracking, scratching, and wear, with colors that remain vibrant and durable. It's 10 times more durable than liquid coatings.
- 5-Speed Upgrades: Tailor your powder coating for different workpieces with precise voltage adjustment ranging from (30/35/40/45/50)KV and 5-speed settings. Our powder coating gun provides uniform coatings. It is suitable for various applications, including metals, automotive parts, furniture, construction materials, fences, and pipes, protecting metals from corrosion.
- User-friendly Dual Switches: Equipped with both foot pedal and button dual switches, this powder coating equipment allows for convenient on/off operation without the need for bending. It can enhance work efficiency and comfort during the coating process.
- 2 Powder Bottles and Nozzles: Easily switch between colors without the hassle of cleaning between powder changes. Each bottle is dedicated to a specific color. This powder coating kit reduces the risk of color contamination due to incomplete cleaning and significantly improves work efficiency.
- Easy Portability: Oure electrostatic powder coating machine comes with a carrying handle for effortless mobility, making it ideal for large spray areas and quick transitions between various workplaces. Whether in an auto repair shop, shipyard, home DIY, or garden, it enhances flexibility in powder coating tasks.
Choosing a coating for the electrical job
| Need | Suitable direction | Important limit |
|---|---|---|
| Appearance, corrosion protection, or structural finish without a dielectric requirement | Ordinary decorative powder; keep electrical contacts separate or mask them. | Do not assume the cured surface conducts or has a certified insulation rating. |
| Electrical isolation of a conductor | Purpose-made dielectric powder with supplier data for thickness, cure, breakdown, resistivity, and aging. | Dielectric strength alone does not establish a safe working voltage or whole-assembly rating. |
| Controlled static-charge dissipation | ESD-dissipative powder specified to a resistance range and test method. | It does not replace protective-earth bonding or prove EMI continuity. |
| Conductive coated surface | Specialty conductive powder with surface-resistance data under the required measurement conditions. | Lateral surface conductivity does not guarantee reliable contact through to the substrate. |
| Protective-earth or low-impedance RF continuity | Designed bare contact lands, bonding hardware, jumpers, or conductive gaskets, then assembly testing. | Do not rely on an ordinary coating or unvalidated fastener penetration. |
For insulation grades, supplier data are available for products such as Resicoat EL; one product datasheet specifies 100–300 µm while a busbar product example specifies 200–300 µm. These are product-specific recommendations, not general powder-coating targets. Request the current datasheet for the precise grade and confirm the qualification fits the actual service.
Why thickness, cure, and exposure matter
Thickness influences breakdown distance, resistance, capacitance, heat transfer, dimensional fit, and a fastener’s ability to reach metal. More coating can improve an ideal film’s voltage margin, but it can also increase thermal resistance, interfere with joints, and cause fit problems. It does not compensate for defects or poor cure. ASTM identifies film thickness as a factor affecting powder-coating physical and appearance properties in D7378.
Measure actual thickness on the relevant substrate and geometry. ISO 2360:2017 covers nondestructive measurement of nonconductive coatings, including powder coatings, on nonmagnetic conductive metals: ISO 2360. Flat coupons alone may not represent edges, holes, seams, recesses, or mesh. Deep recesses and inside corners can receive uneven deposition because electrostatic charge repels powder from already coated areas; Fusecoat’s application discussion describes this Faraday-cage effect.
Cure must follow the powder supplier’s time-at-object-temperature requirements, not simply the oven-air setting. Under-cure can compromise mechanical integrity, adhesion, chemical resistance, and electrical performance; excessive heat may damage resin or substrate or affect dimensions. Moisture, salts, oils, dust, and other contamination can create surface leakage paths. Thermal cycling, abrasion, chips, and cracks can expose metal, create local breakdown sites, or trap conductive contamination. Galvanized or plated surfaces also require suitable preparation: ASTM D7803 notes that preparation variation can produce different galvanized surface conditions before powder coating.
Quick wins for a faster PC:
Clear out junk files and repair common Windows errorsFree Scan →Scan for outdated or missing drivers - takes under a minuteDriver Scan →How to test a coated metal part
| Question | Measurement or method | What to record |
|---|---|---|
| Is the film thick enough and uniform? | Validated coating-thickness method; ISO 2360 applies to nonconductive coatings on nonmagnetic conductive metals. | Substrate, locations, geometry, instrument, and measured thickness. |
| Does the surface conduct or dissipate charge? | Defined surface-resistance test; IGP’s guidance explains the importance of electrode contact. | Electrode geometry and force, spacing, voltage, temperature, humidity, cleanliness, and conditioning. |
| What are the coating material’s electrical resistance properties? | ISO 15091:2019 addresses conductivity and resistance of coating materials and permits resistivity calculation. | Method and specimen conditions; this is not a finished-part bond test. |
| Does the film withstand the required electric stress? | Dielectric withstand or breakdown test at specified conditions; ASTM D7895/D7895M evaluates thermal endurance of insulating powders on steel by aging and measuring time to dielectric breakdown at a specified proof voltage. | Voltage, geometry, thickness, cure, conditioning, and acceptance criteria. |
| Is the finished assembly grounded? | Ground-bond or continuity test on the assembled product. | Actual path, joints, assembly torque, environmental exposure, and applicable standard. |
| Will insulation persist in service? | Thermal, humidity, chemical, and mechanical aging followed by electrical retest. | Exposure profile and results at vulnerable edges and interfaces. |
See ISO 15091 for coating material resistance methods and ASTM D7895/D7895M for thermal endurance testing. A generic multimeter can mislead: its test voltage may be too low, or a sharp probe may puncture the film. For finished-product grounding, test the full assembly across doors, bolted joints, and removable panels, including after vibration, humidity, corrosion, or other relevant exposure.
Design checklist before coating
- Define whether the requirement is insulation, ESD dissipation, surface conductivity, protective grounding, EMI continuity, or some combination.
- Mark ground pads, bonding points, test points, hinges, threaded interfaces, mating surfaces, and thermal contact areas on the drawing.
- Specify powder grade, substrate preparation, cured thickness window, cure schedule at part temperature, and acceptance tests.
- Check corners, edges, recesses, and holes for coverage and dimensional interference.
- Validate the actual joint or assembly after coating and after the environmental exposures relevant to service.
- Use the applicable electrical-safety or product standard for the product category and jurisdiction; do not turn a material datasheet figure into a product rating.
For insulating systems on steel, ASTM D7895/D7895M evaluates thermal endurance by aging coated specimens and determining time to dielectric breakdown; it is not a substitute for qualification of every finished geometry. Magnetic assemblies may intentionally use insulating coatings between conductive components; any dimensional, thermal, or electrical-loss effects there require application-specific evaluation.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

