
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
iTechGuides is reader-supported. When you buy through links on our site, we may earn an affiliate commission. As an Amazon Associate I earn from qualifying purchases. Learn more
For most 3D-printed RC aircraft, start with the filament and print profile specified by the aircraft designer. LW-PLA is often used for airframes designed around low mass; PETG is a better fit for parts specifically called out for toughness or heat resistance; standard PLA can work where the design permits it and heat, sunlight and impact are manageable. These are not interchangeable whole-aircraft recipes: material changes affect part mass, fit and potentially the aircraft’s centre of gravity and structural performance.
PLA vs. LW-PLA vs. PETG: which is best for an RC aircraft?
The best choice depends on the part, the aircraft design and the filament’s printing behavior—not just the polymer name. Use this as a starting point, then follow the model’s own material call-outs.
| Need or constraint | Best starting point | What to check |
|---|---|---|
| Low-mass airframe in a design made for it | LW-PLA | Use the exact filament profile and calibrate the finished part’s mass. Foaming behavior varies by product. |
| A specified part needing greater toughness or heat resistance | PETG | Use it where the designer calls for it; its extra mass and different print behavior make it an unsuitable automatic airframe substitute. |
| Accessible, comparatively straightforward printing | PLA | Confirm the design permits it and account for heat, sun and impact exposure. |
Eclipson lists PLA, tough PLA, PETG and LW-PLA among materials used for its aircraft, reflecting that different parts can need different properties. Its recommendations are design-specific, not a universal material specification: Eclipson’s filament comparison.
Quick wins for a faster PC:
Scan for outdated or missing drivers - takes under a minuteDriver Scan →Clear out junk files and repair common Windows errorsFree Scan →Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Why aircraft designs use different materials for different parts
An airframe is not a single test specimen. Thin skins, wings, fuselage sections, motor mounts and bulkheads have different loads, geometry and exposure. Part mass affects the aircraft’s total weight and centre of gravity; print orientation and layer bonding affect how a printed part handles loads. A material swap can therefore alter more than the part’s nominal strength.
#1 Best Overall

- [Excellent PETG Filament]Our PETG combines the benefits of PLA and ABS to reach Eco-friendly and odorless performance. This PETG Filament is feature in good toughness to avoid cracking and warping, enbale excellent 3D printing.
- [Toughness-enhanced PETG] Our PETG filament choose durable and strong material that delivers excellent clarity, light transmission, and a glossy finish. It is recommended to use a printing temperature of 220-250°C and a base plate temperature of 70-80°C for better printing results.
- [Tangle-Free & Neatly Wound] We ensure that every PETG filament is tightly and neatly wrapped by utilizing full mechanical winding, which effectively minimizes tangles, filament snapping, and line breakage.
- [No Clogging & No Bubbles] Our filaments are thoroughly dried and carefully vacuum sealed to protect them from moisture and dust, which ensures that there will be no issues with clogging or bubbling during printing. Our PETG is designed to be perfectly compatible with the majority of 1.75mm FDM 3D printers, especially suitable for Creality 3D Printers!
- [High Precision & Consistent Performance]Our PETG filament boasts a diameter of 1.75mm, ensuring utmost accuracy with a tolerance of only +/- 0.03mm. With strict quality control and impeccable dimensional precision, our PETG filament guarantees a smooth and steady feeding during printing.
WUDFLY’s profile documentation uses foaming LW-PLA for the main airframe and PETG for specified structural parts, including a motor mount. It says its profiles were developed using a Bambu Lab X1 Carbon and ColorFabb LW-PLA, and ties settings to its aircraft files and reference part masses. That is an example of a designer’s workflow, not a recipe to apply to other aircraft. See WUDFLY’s print profiles.
LW-PLA: light when the filament and profile are matched
LW-PLA is not one uniform process. Some products foam actively in the hot end; others use a different, stabilized foaming behavior. Consequently, a profile, temperature or flow value that works for one product may not work for another.
Rank #2
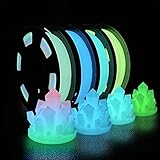
- 🌟Are the regular 3D printer filament colors too monotonous? Better to try Glow in The Dark Filament,which appears white at day, but emits light at night. Making it perfect for creation needing low-key, rich and enigmatic appearance
- 🌟What is an excellent PLA filament for you? A filament that can glow in the dark? Odorless, Clog-Free, Bubble-Free & Easy-to-use? No odor and low warpage during printing? High toughness and excellent strength?How about something that combines the functionality of all of the above
- 🌟Safe to use and made of natural materials,reliable and durable. CE, RoHS certificated by authority,. The phosphorescent substance in PLA Filament absorbs light energy and emits light in the dark. In order to get better results, we recommend that the model be exposed to sunlight or UV light for 15 minutes
- 🌟You don’t have to worry that it will be incompatible with your 3D printer — 1.75 mm in diameter, dimensional accuracy +/- 0.03 mm. It works perfectly with most FDM 3d printers on the market (For example MK3, Ender 3, Monoprice FlashForge, etc)
- 🌟Vacuum sealed packaging: iSANMATE 3d filament is carefully vacuum packed with desiccant to maintain the performance of PLA filament. And keep it dry to prevent dust and foreign matter from entering to prevent nozzle clogging
Active-foaming LW-PLA
For the material covered in its guide, Prusa describes expansion during printing, with the amount depending on nozzle temperature and print speed. Its guidance gives a 210–250 °C nozzle range and says expansion can reach 2.3–3 times the original size; it also lists a 65% weight reduction and 270% volume increase for that material and process. These are product- and process-specific figures, not promises for all LW-PLA. Prusa warns that the material can ooze or string more and recommends calibrating extrusion multiplier and temperature. Its highest cited expansion is around 240–250 °C. See Prusa’s LW-PLA guidance.
Other LW-PLA formulations
Polymaker says its PolyLite LW-PLA uses Stabilized Foaming technology, re-foams after extrusion, decreases density by 30%, and can be printed with regular PLA settings at 190–210 °C. This differs from active foaming in the nozzle and is a practical reason to check the particular spool’s documentation rather than assume one LW-PLA profile fits all. See Polymaker’s PolyLite LW-PLA product information.
Rank #3

- [Excellent Clear Petg]Our PETG combines the benefits of PLA and ABS to reach Eco-friendly and odorless performance. This transparent Filament is feature in good toughness to avoid cracking and warping, enbale excellent 3D printing.
- [Toughness-enhanced PETG] Our PETG filament choose durable and strong material that delivers excellent clarity, light transmission, and a glossy finish. It is recommended to use a printing temperature of 220-250°C and a base plate temperature of 70-80°C for better printing results.
- [Tangle-Free & Neatly Wound] We ensure that every PETG filament is tightly and neatly wrapped by utilizing full mechanical winding, which effectively minimizes tangles, filament snapping, and line breakage.
- [No Clogging & No Bubbles] Our filaments are thoroughly dried and carefully vacuum sealed to protect them from moisture and dust, which ensures that there will be no issues with clogging or bubbling during printing. Our PETG is designed to be perfectly compatible with the majority of 1.75mm FDM 3D printers.
- [High Precision & Consistent Performance]Our PETG filament boasts a diameter of 1.75mm, ensuring utmost accuracy with a tolerance of only +/- 0.03mm. With strict quality control and impeccable dimensional precision, our PETG filament guarantees a smooth and steady feeding during printing.
Flightory likewise distinguishes prefoamed filament, whose volume is set during manufacturing and which it says prints at standard flow, from active-foaming filament that expands in the nozzle and uses reduced flow in its profiles. It publishes settings by brand for its own aircraft. Follow the profile for the exact aircraft and filament: Flightory’s print settings.
PETG: use it where toughness or heat performance is specified
PETG is a reasonable choice when a particular aircraft part calls for more tenacity or temperature resistance than the design assigns to PLA. Prusa describes PETG as tough, with good layer adhesion, and suitable for many exterior applications below 80 °C. That general material guidance does not establish a safe operating temperature for a particular aircraft part. PETG also tends to string, performs less well than PLA on bridges and overhangs, adheres strongly to print sheets and requires a heated bed. See Prusa’s PETG guide.
Rank #4

- ①【SUNLU PLA 3D Printer Filament】PLA material is the perfect choice for 3D printing enthusiasts! SUNLU PLA filament is reliable, versatile, and easy to use. No clogs, bubbles, or tangles, its excellent layer adhesion ensures high-quality prints every time. Ideal for beginners and experienced users.
- ②【Neatly Wound 3D Filament Spool】SUNLU's self-developed neat winding device ensures that the filament is easy to use, with a 100% neat rate that reduces the risk of tangles and jams, and provides a smoother and more efficient 3D printing experience.
- ③【PLA Filament 1.75 mm】SUNLU 3D printer filament dimensional Accuracy +/- 0.02mm. SUNLU filament has wide compatibility due to the small diameter error, making it suitable for almost all 1.75mm FDM 3D printers.
- ④【Filament Spool Diameter】Spool Diameter: 8.00", Spool Width: 2.50", Spool Hub Hole Diameter: 2.20". The size of the SUNLU filament spool is suitable for hanging on a lot of FDM 3D printers.
- ⑤【PLA Recommend Settings】To achieve the best printing results with SUNLU PLA filament, we recommend printing at a nozzle temperature of 200-230°C, a bed temperature of 50-65°C, and a printing speed of 50-100mm/s.
WUDFLY names motor mounts and bulkheads as examples of parts for which aircraft instructions may specify PETG, and warns against PLA in heat-loaded mounts. Use the aircraft’s call-out rather than upgrading every component to PETG: its higher density can work against the low-mass goal, and its print behavior may require different tuning.
PLA: easy to print, but check heat, sun and impact
PLA is typically accessible and straightforward to print. Prusa describes it as easy and inexpensive, with low warping, but says it softens and deforms above 60 °C, degrades under UV exposure and may break along layers or into shards on impact. A plane left in a hot vehicle, exposed to direct sun or subject to rough landings may face conditions that matter to those limits. These are material cautions, not proof that PLA is unsuitable for every aircraft: designers may specify it for particular geometries and uses. See Prusa’s PLA guide and Eclipson’s material recommendations.
How to choose and validate a filament for your model
- Read the aircraft instructions first. Identify the specified filament for each part and any supplied slicer profile. Do not substitute PETG or PLA across the whole aircraft based only on a general material comparison.
- Check the exact spool’s behavior. For LW-PLA, establish whether it actively foams or uses another approach, then use the filament maker’s settings and the aircraft designer’s profile as applicable.
- Print a reference part and compare mass and fit. WUDFLY advises checking its package’s part masses and fitment; Flightory says its aircraft instructions specify part settings. A deviation can affect balance, clearances or assembly.
- Inspect the relevant failure risks. Consider layer direction and adhesion, wall and infill settings, reinforcement, expected loads and landing impacts. A polymer label alone cannot establish part strength.
- Check operating and storage conditions. Consider hot electronics, a parked vehicle, sunlight, moisture and expected outdoor exposure against the limits of the chosen material and design.
- Recheck the assembled aircraft before flight. WUDFLY calls for verification of part mass, fitment, electronics clearance, centre of gravity and airworthiness. Its guidance is not independent flight-safety certification; a filament datasheet alone cannot validate an aircraft.
What printed-sample measurements do—and do not—show
A 2025 Stanford 3D PAC technical report lists measurements from printed samples: PLA density 1.213 g/cm³ and tensile strength 23.333 MPa; PETG density 1.202 g/cm³ and tensile strength 16.667 MPa; and ColorFabb LW-PLA density 0.553 g/cm³ and tensile strength 4.167 MPa. These are sample measurements, not universal filament constants or manufacturer datasheet values. Printing method, orientation and test conditions limit how directly they transfer to a specific aircraft part. The report is Stanford 3D PAC’s 2025 technical report.
Eclipson separately claims 60% higher impact resistance for PETG than PLA on its filament comparison page, while noting that properties vary by manufacturer, settings and environment. It also describes LW-PLA density as half that of the PLA in its comparison and says its flow is 50%, explaining that as equivalent material consumption of 1 kg LW-PLA to 2 kg PLA. Treat those as Eclipson’s comparisons, not universal properties of all brands or foaming formulations: Eclipson’s filament comparison.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

