
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
Non-destructive testing (NDT) lets oil-and-gas teams inspect pipelines, tanks, pressure vessels, welds, and offshore structures without damaging the component being examined. The right method depends on what needs to be found, the material and surface condition, access, and the result required; no single technique is a shortcut for all the others.
What is non-destructive testing in the oil and gas industry?
NDT examines a material, component, or structure while leaving it usable after inspection. It is also called nondestructive evaluation (NDE) or nondestructive inspection (NDI). The term covers methods that produce different kinds of information: a visible surface indication, a wall-thickness measurement, an image of internal structure, or a signal associated with active damage. ASNT describes six widely used methods: visual, ultrasonic, radiographic, magnetic particle, liquid penetrant, and electromagnetic testing (ASNT overview; method overview).
These examinations support inspection of different assets for different reasons. For example, pipeline programs may use visual, ultrasonic, and radiographic testing; tank integrity work may include visual and magnetic particle testing; and pressure-vessel condition monitoring may use acoustic emission or electromagnetic techniques. Weld inspection is another central application. These are examples of uses, not a universal inspection schedule or a prescription for every asset (ASNT energy applications).
Which NDT methods are used, and what can each reveal?
Visual testing (VT)
Visual testing begins with direct observation, sometimes aided by cameras or other optical equipment. Robotic crawlers and cameras can help examine pipelines, while visual checks also feature in tank integrity work. VT can identify conditions that are visible from the inspection vantage point, but a clear-looking surface does not establish that hidden internal discontinuities are absent (ASNT energy applications; ASNT overview).
#1 Best Overall

- ULTRASONIC THICKNESS GAUGE – INDUSTRIAL-882 FOR MATERIAL INSPECTION – Industrial-882 ultrasonic thickness gauge is designed for measuring the thickness of solid materials when access is available from one side only. It is commonly used for inspection of steel structures, pipes, tanks and metal components during maintenance and technical inspection.
- NON-DESTRUCTIVE ULTRASONIC MEASUREMENT METHOD – The device measures thickness by sending an ultrasonic signal through the material and calculating thickness from the echo return time. This allows technicians to evaluate metal thickness without cutting, drilling or damaging the inspected component.
- WIDE MEASUREMENT RANGE FOR INDUSTRIAL APPLICATIONS – The measuring range of 0.039–8.858 in (1–225 mm) allows inspection of thin sheets, metal plates, machine parts and pipeline walls. The device can be used in maintenance inspections, industrial diagnostics and production quality control.
- ADJUSTABLE SOUND VELOCITY FOR DIFFERENT MATERIALS – Sound velocity can be adjusted to match different materials such as steel, aluminum, copper, plastic or glass. This helps obtain stable readings when measuring different types of materials in technical inspection tasks.
- COLOR LCD DISPLAY WITH CLEAR READINGS – The device features a color LCD display that allows users to read measurement values clearly in workshop and industrial environments. The interface allows convenient navigation when adjusting measurement parameters.
Ultrasonic testing (UT)
UT sends high-frequency sound into a material and interprets returning signals. It can measure wall thickness and detect internal discontinuities, making it useful for corrosion assessment in pressure equipment and piping, crack detection in in-service equipment, and weld inspection during fabrication (ASNT ultrasonic testing).
UT is a family of techniques rather than one instrument or setup. Conventional thickness measurement, phased-array UT (PAUT), time-of-flight diffraction (TOFD), guided-wave testing, and electromagnetic acoustic transducer (EMAT) approaches address different configurations. Guided waves can screen remote or difficult-to-access pipeline areas, but interpretation is complex and defect sizing can be uncertain; additional methods may be needed when accurate sizing matters. EMAT can help on rough, hot, or coated surfaces where conventional couplant-based UT is difficult, but it requires specialized equipment (ASNT ultrasonic testing).
An ultrasonic thickness gauge is for a defined thickness-measurement task, not a complete inspection program. The probe, calibration or reference practice, procedure, material, geometry, and interpretation all affect whether a measurement is suitable for its intended use.
Rank #2

- Entirely Non-Destructive: You can measure material thicknesses from 0.039 to 11.811 inches (steel) in 0.5 seconds, with a resolution of up to 0.0003 inches, and an accuracy of ±(0.5% H+0.001 inches). Two units switchable (mm/in)
- Adjustable speed of sound: Adjustable from 1000-9999 m/s, with 12 material presets and customizable settings to ensure accurate measurements
- Multifunctional: This ultrasonic thickness gauge features a color LCD backlight, enabling it to be used in all light conditions. , Min/Max/average mode, customized sound velocity presets, data storage, high & low limit alarms, low battery indicator, auto power off, automatic probe recognition features and support the connection of computer software for data recording and statistical analysis
- Long Battery Life & Portability: This handheld ultrasonic thickness gauge weighs only 5.57 oz, making it easy to carry and operate. Equipped with a built-in 1000mAh rechargeable battery, it delivers up to 8 hours of continuous use. The ergonomic rubber housing ensures a comfortable grip while offering enhanced protection against impacts and abrasions
- Versatile: PM1201 ultrasonic thickness gauges are used for measuring Metal and Nonmetal materials i.e. Plastic, Rubber, Caramics, Steel, PVC, Glass Plates and Pipes. They can be widely used in the fields such as manufacturing and metal processing, etc. It can also make detection on various kinds of pipes and pressure vessels of the manufacturing facilities about their thickness lossing after corrosion
Radiographic testing (RT)
Industrial radiography uses X-rays or gamma rays to create an image of internal component conditions. It is used to examine pipeline, storage-tank, and offshore-structure components, including welds and internal defects. A radiographic examination can leave a lasting inspection record; image-quality evidence may also be included when image quality indicators are used (ASNT radiographic testing; ASNT energy applications).
Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchPC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11RT uses ionizing radiation. The examination therefore needs the controls and legal requirements established by the applicable jurisdiction and procedure; a general description of the method cannot determine those requirements for a particular job (ASNT radiographic testing).
Magnetic particle testing (MT)
MT magnetizes a part made of ferromagnetic material and applies dry or suspended magnetic particles. Indications can reveal surface and near-surface discontinuities. Oil-and-gas applications include pipelines, pressure vessels, storage tanks, drilling tools, and rigs. Because the method depends on magnetization, it is not a general choice for nonferromagnetic alloys or components (ASNT magnetic particle testing).
Rank #3

- PROFESSIONAL THROUGH-COATING INSPECTION — Echo-Echo mode allows measurement of base metal thickness without removing paint or protective layers. Ideal for coated pipelines, storage tanks, marine structures and painted industrial equipment where surface preparation is not possible.
- VERSATILE MODE SELECTION FOR REAL TASKS — Pulse-Echo mode is designed for direct thickness measurement on uncoated materials including cast iron and rough industrial surfaces, supporting maintenance, repair and mechanical inspection workflows.
- PRECIOUS METAL VERIFICATION FUNCTION — VERI mode analyzes internal ultrasonic response to help assess material consistency, making it useful for checking gold and silver bars, coins and other high-value metal items.
- ENGINEERED FOR CORROSION MONITORING — Suitable for evaluating wall loss in pipes, pressure vessels, structural steel and machinery components during preventive maintenance and condition assessment programs.
- ADJUSTABLE SOUND VELOCITY CONTROL — Supports custom velocity configuration for different materials, enabling accurate thickness measurement across steel, aluminum, copper and other industrial metals.
Liquid penetrant testing (PT)
PT uses a penetrant that enters defects open to the surface of a solid, nonporous material. A developer draws the penetrant back out so the indication can be seen. The surface must be accessible and suitably clean, and the method does not provide an image of internal conditions like UT or RT. Field kits commonly include cleaner, penetrant, and developer, but the procedure and material compatibility govern their use (ASNT liquid penetrant testing).
Electromagnetic testing (ET)
Electromagnetic testing includes eddy-current approaches, which induce currents in conductive materials and detect changes associated with material conditions or discontinuities. Specialized approaches include remote-field testing for ferromagnetic tubes and pulsed eddy current for corrosion under insulation. The right technique and probe depend on the material, geometry, target, and depth being examined (ASNT electromagnetic testing).
Recommended Free Tools
Other application-specific methods
Acoustic emission can support pressure-vessel monitoring, while thermal or infrared inspection can identify hot spots in electrical systems or turbines. These methods add information for particular monitoring or thermal questions; they do not replace choosing a suitable examination for a specific weld or wall-loss concern (ASNT energy applications).
Rank #4

- ULTRASONIC MEASUREMENT: Ultrasonic Thickness Gauge 882X offers precise measurement of various homogeneous materials, including metals like steel, aluminum, and copper, as well as plastics, ceramics, and glass. Utilizing advanced ultrasonic wave technology, it ensures accurate and reliable thickness assessments of material.
- TECHNICAL PARAMETERS: Ultrasonic Thickness Gauge Industrial-882X delivers a broad measurement range of 0.039 to 11.811 inches (1 mm to 300 mm) for 45# steel, ensuring versatility for industrial applications. With an impressive resolution of 0.001 inches, it provides precise and reliable thickness measurements for professional use.
- CALIBRATION & SETTINGS: Ultrasonic Thickness Gauge Industrial-882X ensures accuracy with easy calibration using a reference block and customizable sound velocity settings. With a sound speed range of 0.039–0.393 in/μs (1000–9999 m/s), it adapts seamlessly to various materials for precise measurements.
- HANDHELD & COMFORTABLE: The Ultrasonic Thickness Gauge Industrial-882X features a compact, handheld design for effortless portability. Powered by a high-speed microprocessor, it ensures efficient and reliable operation in any industrial setting.
- ADVANCED DISPLAY: Ultrasonic Thickness Gauge Industrial-882X boasts an HD color screen with adjustable backlight brightness for optimal visibility in any environment. Customize the interface with a selection of vibrant colors, including blue, orange, green, purple, and grey, for a personalized user experience.
How do you choose an NDT method?
Start with the inspection question, then check whether the method can answer it under the actual material and access conditions. A method that can detect an indication may not provide the sizing accuracy, coverage, or record a project needs.
- Define the target. Decide whether the concern is a visible condition, a surface-breaking flaw, a near-surface discontinuity, an internal flaw, wall loss, or a signal associated with active damage.
- Identify the material and geometry. MT requires ferromagnetic material; PT requires an accessible, suitably clean, nonporous surface; ET depends on conductivity and probe fit; and UT or RT setups must suit the component geometry.
- Assess access and surface state. Consider whether the inspection can reach the needed area, whether the surface is coated or insulated, and whether temperature or roughness affects the technique.
- Specify the result needed. Screening, location, thickness, sizing, internal imaging, and a permanent record are different objectives. For instance, guided-wave testing may screen remote pipeline sections, but uncertain sizing can call for follow-up examination.
- Apply the governing procedure and acceptance criteria. The asset requirements, applicable code basis, and jurisdiction matter. ASNT’s UT discussion references ASME Boiler and Pressure Vessel Code Section VIII and API 510 and API 570 for pressure-vessel and piping inspection; that reference alone does not establish which edition or legal requirements apply to a specific project (ASNT ultrasonic testing).
Method selection and application belong under the relevant qualified personnel, procedure, and acceptance criteria. In practice, methods may be combined: one can screen or locate a concern, while another provides the kind of sizing or confirmation the inspection objective requires.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.Which NDT method is used for pipeline inspection?
There is no single pipeline method for every inspection question. Visual testing can examine accessible surfaces or use cameras and robotic crawlers; UT can measure thickness or assess internal discontinuities; and RT can image internal conditions in components such as welds. Guided-wave UT can screen areas that are difficult to access, but accurate sizing may require verification with another technique. The chosen method depends on the target, pipe material and configuration, access, and required result (ASNT energy applications; ASNT ultrasonic testing; ASNT radiographic testing).
Best Value
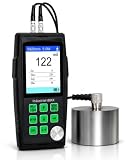
- PROFESSIONAL MATERIAL EVALUATION: Engineered for high-precision material thickness assessment in manufacturing, industrial quality control, and structural verification applications. Expertly measures base material thickness for steel, iron, aluminum, brass, glass, PVC, and other homogeneous solid materials, ensuring adherence to manufacturing and assembly tolerances.
- PRECISION MEASUREMENT PERFORMANCE: Delivers a measurement range of 0.033–15.75 inches (0.85–400 mm) with a digital display resolution of 1 mils or 0.01 mm. Measurement accuracy is controlled at ±(1%H+0.1) mm, providing dependable data for engineering inspection workflows and dimensional quality assurance.
- EXPANDABLE PROBE ARCHITECTURE: Includes the standard 5MHzΦ10 probe for everyday measurements and supports specialized 7.5MHzΦ6, ZW5P (up to 572°F / 300°C), 2.5MHzΦ12, and 2.0MHzΦ22 probes, providing optimized performance for thin materials, high-temperature surfaces, thick steel, cast iron, coarse-grain metals, and heavy industrial inspections.
- INTELLIGENT SOUND VELOCITY CALIBRATION: Supports Zero Calibration, Manual Velocity Entry, and Automatic Sound Velocity Calculation using a reference sample of known thickness. Instead of searching material velocity tables, simply calibrate on a known sample and the gauge automatically determines the correct sound velocity, providing faster setup, improved accuracy, and more reliable measurements across different homogeneous materials.
- PC DATA EXPORT FOR REPORTING – Transfer saved thickness readings to a computer for documentation, report generation, batch tracking, and long-term measurement records. Ideal for production logs, workshop documentation, material verification, and internal quality control processes.
What is the difference between ultrasonic and radiographic testing?
UT uses sound waves and interprets their reflections or other signals; depending on the setup, it can measure wall thickness or detect internal discontinuities. RT uses X-rays or gamma rays to create an image of internal conditions and can produce a lasting record. They therefore provide different evidence and have different access, equipment, and safety considerations. Neither is automatically the better option: the component, inspection target, procedure, and result required determine the appropriate choice (ASNT ultrasonic testing; ASNT radiographic testing).
Can NDT find corrosion or cracks without taking equipment apart?
Often, yes—but the method must suit the defect and the accessible inspection area. UT can measure wall thickness for corrosion assessment and detect internal discontinuities; MT and PT can reveal certain surface or near-surface indications when their material and surface requirements are met. RT can image internal conditions. The result only supports conclusions within the coverage and capabilities of the examination performed; no one method establishes that every part of a complex asset is free of defects (ASNT ultrasonic testing; ASNT magnetic particle testing; ASNT liquid penetrant testing; ASNT radiographic testing).
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

