
The Tool Desk
Outbyte Driver Updater FREEFix the driver behind crashes, sound loss and screen glitchesFind Drivers →Outbyte PC Repair FREEClear out junk files and repair common Windows errorsFree Scan →iTechGuides is reader-supported. When you buy through links on our site, we may earn an affiliate commission. As an Amazon Associate I earn from qualifying purchases. Learn more
When a warehouse robot, conveyor, shuttle, or automated picking workflow stops, treat the area as hazardous until your site procedure confirms otherwise. Keep people outside the motion zone, identify whether the event involves an injury or collision, capture the system’s exact alarm, and do not reach into equipment, remove guards, bypass interlocks, or try an improvised reset. Safe servicing requires trained, authorized workers using the installation’s energy-control and manufacturer procedures.
1. Make the area safe before diagnosing anything
A stopped machine is not proof that electrical, pneumatic, hydraulic, gravitational, or mechanical energy has been isolated. A controller may still command motion, a conveyor may restart when an upstream condition clears, and a suspended load or compressed mechanism may move without warning.
Stop and protect people
- Keep operators, visitors, and unassigned maintenance staff outside the robot cell, conveyor hazard zone, pallet-transfer area, and any marked exclusion boundary.
- Use the site’s emergency and incident procedure if anyone is injured, trapped, struck, exposed to a pinch point, or involved in a collision.
- Do not step through a gate, cross a conveyor, enter a robot envelope, or approach a fallen load merely because motors appear quiet.
- Do not defeat a gate switch, light curtain, scanner, emergency stop, guard, software permission, or other protective device to make the system run.
If access, jam removal, guard removal, adjustment, or inspection inside a safeguarded area is required, stop operator-level troubleshooting. The work belongs to trained and authorized personnel following the employer’s written energy-control program and the equipment manufacturer’s service instructions.
Quick wins for a faster PC:
Repair Windows errors before they cause bigger problemsFix Now →Fix the driver behind crashes, sound loss and screen glitchesFind Drivers →Clear out junk files and repair common Windows errorsFree Scan →Classify the event without entering the hazard
| What you observe | What it may indicate | Safe response |
|---|---|---|
| Emergency stop, protective scanner, open gate, or safety-controller message | A safety event or a condition that prevents motion | Keep clear, record the message, and follow the approved safety-event recovery procedure |
| One robot or station is stopped while surrounding equipment remains available | A local controller, tool, sensor, or station fault | Collect the local alarm and affected-zone information; escalate if guarded access is needed |
| Several machines stop together | A shared conveyor, controller, network, power, or upstream/downstream condition | Record the sequence and common equipment; do not reset multiple systems blindly |
| Product has fallen, shifted, or visibly blocks a route | A jam or obstruction with stored or unexpected energy | Keep hands and tools out; use the site’s lockout and jam-clearing procedure |
These categories help you decide who should respond; they are not a universal diagnosis. Every integrated installation exposes different alarms and recovery permissions.
#1 Best Overall

- LOCKOUT TAGOUT KIT: Lockout pouch is made of heavy duty nylon with metal belt loops for convenient tagging on the go, Compliant with OSHA's Lockout Standard
- SAFETY PADLOCKS: The personal lockout kit contains two keyed different padlocks for reliable lockout safety, the key is one use one spare.
- LOCKOUT DEVICES: Kit contains 3 clamp-on circuit breaker lockout, 3 Universal Multi- Pole Breaker ,3 different size lockout hasps,15 heavy duty lockout tags,4 keyed-different safety padlocks:Stainless Steel Lock Beam, with PA Shell ,Vertical Clearance: 1-1/2”, 38mm,Horizontal Clearance: 4/5”, 20mm ,Shackle Dia.: 1/5”, 6mm ,Body Size: 1-4/5” x 1-2/5”, 45 x 37mm
- OSHA COMPLIANT LOCKOUT KIT: Compliant with OSHA's Lockout Standard designed to address risk and safety tagging in any facility
- We have confidence in our product. If you are not satisfied with our products, please contact us and we will reply to you within 24 hours.
2. Record exactly what the system reports
Before acknowledging or clearing an alarm, preserve the information that can disappear from a display. This is practical diagnostic discipline, not a substitute for the site’s formal incident-reporting requirements.
- Write down the exact alarm text and numeric code, including capitalization, punctuation, and any subcode.
- Record the time, date, shift, robot or conveyor identification, and the station or zone where motion stopped.
- Note what the process was doing: picking, placing, replenishing, transferring a tote, charging, homing, or waiting for another device.
- Record whether the stop affects one machine, a cell, a conveyor segment, or the entire line.
- Capture any visible status shown by the human-machine interface, safety controller, conveyor controller, warehouse-management interface, or supervisory system.
- Write down recent changes: a product or carton change, tooling adjustment, software or recipe deployment, maintenance activity, power interruption, network work, or moved guarding.
- Preserve photographs or screen captures only from a safe location and in accordance with site privacy and security rules.
Do not repeatedly acknowledge an alarm before recording it. Acknowledge buttons can remove the first fault from the active display while the underlying condition remains.
3. Check only safe, external conditions allowed by procedure
An operator may be able to inspect the surroundings without touching machinery. Stay outside the protected area and obey floor markings, barriers, and local instructions.
Recommended Free Tools
- Look for fallen cartons, totes, pallets, labels, wrap, or product outside the normal travel path.
- Check whether a pallet, tote, or container is visibly mispositioned at an infeed or transfer point.
- Look for an obvious external obstruction at a conveyor entrance or discharge without reaching between rollers, belts, chains, guides, or transfers.
- Observe whether a photoelectric sensor appears covered, displaced, or blocked from outside the guard. Do not adjust or clean it unless the procedure specifically permits that task.
- Check for a visible open gate, tripped emergency stop, or indicator that can be read without entering the hazard zone.
- Note unusual noise, smell, smoke, heat, leakage, or a damaged cable from a safe distance, then use the emergency procedure for a potentially dangerous condition.
Never clear a jam by pulling product, jogging a belt, pushing a robot arm, or restoring power as a “test.” A blockage can release suddenly, and a control command can produce movement in a different part of the integrated system.
4. Understand what can fail in an integrated picking system
A warehouse robot is part of a system rather than an isolated arm. OSHA’s OSHA Technical Manual – Industrial Robot Systems and Industrial Robot System Safety describes systems that combine a robot, controller, sensors, end-effectors or tooling, power, and associated machinery. A fault at an interface can look like a robot failure even when the arm itself is healthy.
Rank #2

- LOCKOUT TAGOUT KIT: Lockout pouch is made of heavy duty nylon with metal belt loops for convenient tagging on the go, Compliant with OSHA's Lockout Standard
- SAFETY PADLOCKS: The personal lockout kit contains two keyed different padlocks for reliable lockout safety, the key is one use one spare.
- LOCKOUT DEVICES: Kit contain 3 Safety Padlocks with number 1-3, 2 Lockout Hasp ,1 Nylon hasp ,15 Loto Tags, 20 Nylon ties , 1 Lockout Tool Bag
- OSHA COMPLIANT LOCKOUT KIT: Compliant with OSHA's Lockout Standard designed to address risk and safety tagging in any facility
- We have confidence in our product. If you are not satisfied with our products, please contact us and we will reply to you within 24 hours..
Robot and controller
The controller may stop because of a program state, protective stop, position condition, drive fault, or communication with another device. Only the installation’s documentation can define the alarm and the permitted recovery. Do not infer a cause from a generic label such as “servo,” “motion,” or “program” without the model-specific explanation.
End-effector and tooling
Grippers, vacuum equipment, clamps, forks, and tool changers can fail to confirm that a load is present, released, or safely secured. A picking sequence may halt to prevent a dropped item, even though the robot reports no mechanical damage. Tool inspection, adjustment, and testing inside the cell require the approved service method.
Sensors and protective devices
Presence, position, pressure, vacuum, gate, scanner, and light-curtain signals often form permissive conditions. A sensor can be dirty, displaced, blocked, damaged, or correctly reporting that a process condition is unsafe. Do not bridge or simulate a signal to bypass the stop.
Conveyors and transfers
Conveyors, lifts, sorters, and transfer mechanisms can stop because material is jammed, a downstream station is full, a guard is open, or a shared control has removed permission to run. A robot waiting for a tote may therefore be a symptom of a conveyor or upstream problem.
Shared controls and utilities
Power distribution, safety control, industrial networks, compressed air, vacuum, and warehouse-execution interfaces can affect multiple stations. A simultaneous stop across zones is useful evidence, but it is not authorization to open a panel or reset a controller. Qualified personnel must test and restore these systems under site rules.
Rank #3
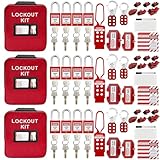
- 1、 What You Get. 3 x Complete LOTO Kits (Each Contains): 4 Safety Padlocks、2 Steel Hasps、1 Nylon Hasp、15 LOTO Tags、20 Cable Ties、1 Big Nylon Pouch、4 clamp-on circuit breaker lockout, 3 Universal Multi- Pole Breaker, 2 Electrical Plug Lockout + SAFBY's 2-Year Support。
- 2、OSHA-Compliant Safety:Meets all lockout/tagout (LOTO) standards for electrical, mechanical and industrial safety,Complete 3-Kit Set Perfect for teams or multiple workstations。Each kit is self-contained with all essential LOTO devices。
- 3、Superior Durability:Reinforced steel hasps withstand tough environments,Weather-resistant tags and nylon components。
- 4、 Clear Hazard Communication:Bright red safety tags with bold warnings,Numbered padlocks for easy identification。
- 5、Convenient Portability:Compact nylon pouch with metal belt loops,Keeps all devices organized and accessible。
5. Use the correct branch for the stoppage
Branch A: a safety device or emergency stop is active
Keep the hazard area clear. Identify the displayed safety message and the affected zone from outside the guard. Follow the site’s procedure for investigating why the device operated. A reset is appropriate only after the cause has been resolved, the area has been inspected as required, all people are accounted for, and the procedure confirms that safeguards are restored.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
Branch B: a single station reports a process fault
Record the code and sequence details, then check permitted external conditions such as a missing tote or visible misalignment. If the next step involves opening a gate, removing a guard, entering the cell, manipulating tooling, or clearing product, refer the job to authorized maintenance or the qualified vendor support channel.
Branch C: a conveyor is jammed or material has fallen
Do not reach into the belt, rollers, chains, transfer points, or drive area. OSHA’s warehouse guidance states: “Conveyors: Inspect conveyors regularly.” It also says, “Ensure that pinch points are adequately guarded,” and recommends developing procedures for locking out conveyors when materials have fallen off or become jammed, with worker training in those procedures.
The authorized worker must identify every energy source, isolate it under the employer’s lockout/tagout procedure, dissipate or restrain stored energy, verify isolation, clear the material, replace guards, and complete the required inspection before release. The exact sequence depends on the conveyor and its integration.
Branch D: several machines stopped at once
Record which zones stopped first and which remained available. Report common alarms, power indications, network status, and upstream/downstream conditions to the control-room or automation team. Avoid cycling power across the line unless the approved recovery procedure explicitly requires it and an authorized person has confirmed the consequences.
Free tools Windows power users keep installed
One-click scans. No signup required.
Rank #4

- COMPLETE ELECTRICAL LOCKOUT KIT: Designed for electricians, maintenance teams, and industrial facilities, this complete LOTO kit includes safety padlocks, breaker lockouts, hasps, tags, ties, and storage bag to manage hazardous energy safely and efficiently.
- 4 KEYED-DIFFERENT SAFETY PADLOCKS: Each lock has a unique key configuration for personal lock control. Durable safety locks help prevent unauthorized equipment operation during maintenance and service procedures.
- UNIVERSAL CIRCUIT BREAKER LOCKOUTS: Includes clamp-on and multi-pole breaker lockout devices designed to fit a wide range of electrical panels, helping technicians handle different lockout applications with one kit.
- MORE COMPLETE LOCKOUT OPTIONS: Includes plug lockout, lockout hasps, safety tags, and nylon ties for electrical equipment isolation, group lockout procedures, and daily maintenance tasks.
- READY FOR INDUSTRIAL USE: Store and organize all LOTO devices in the durable portable bag. Ideal for factories, workshops, electrical rooms, machinery maintenance, and facility safety programs.
6. Know when troubleshooting becomes maintenance
OSHA identifies programming, maintenance, testing, setup, and adjustment as non-routine robot work in which accidents can occur. The distinction is practical: observing a display from outside the hazard area may be operator troubleshooting; opening a guard, entering a cell, clearing a jam, changing tooling, or testing an energized component is maintenance or service work.
For service work, the employer’s energy-control program should define equipment-specific procedures, employee roles, training, periodic inspections, and the steps for shutdown, isolation, verification, and restoration. A lockout/tagout kit is useful only when its locks, tags, devices, and test equipment match the actual energy sources and the site’s written procedure. A kit does not replace training, authorization, or the program itself.
OSHA’s industrial-robot guidance discusses energized troubleshooting only in the context of safeguarded, authorized work. It should not be interpreted as permission for an operator to enter a protected area or defeat a safeguard.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.7. Restore the system through the approved sequence
There is no universal reset sequence for warehouse robots or picking systems. The installation’s manufacturer documentation and site procedure control the order.
- Confirm that the fault condition has been identified and corrected, or that qualified support has authorized the next step.
- Verify that tools, loose product, removed guards, temporary barriers, and personnel are accounted for.
- Confirm that emergency stops, gates, scanners, light curtains, and other safeguards are returned to their required operating state without bypassing them.
- Complete the documented isolation-removal and restart checks if lockout or other energy control was used.
- Use only the reset, homing, recovery, or re-enabling sequence specified for that model and software version.
- Observe the first controlled cycle from the designated safe position. Stop and escalate if the alarm returns, motion is abnormal, the load is unstable, or the process does not match the expected sequence.
- Record the action taken, the result, and any parts, settings, or software changes for the shift handover and maintenance history.
If documentation is missing, the alarm is unexplained, or the system will not meet its normal safeguard checks, leave it unavailable and contact the qualified site automation team or system vendor. “Try another reset” is not a diagnosis.
Best Value

- LOCKOUT TAGOUT KIT: Lockout box is made of 304 steel with PP which is heavy duty and portability, Compliant with OSHA's Lockout Standard
- SAFETY PADLOCKS: The personal lockout kit contains two keyed different padlocks for reliable lockout safety, the key is one use one spare.
- LOCKOUT DEVICES: Kit contains 9 clamp-on circuit breaker lockout, 3 Universal Multi- Pole Breaker ,6 different size lockout hasps, 20 heavy duty lockout tags, 5 keyed-different safety padlocks, 1 plug lock, 1 cable lock, 1 gas valve lockout, 1 ball valve lockout
- OSHA COMPLIANT LOCKOUT KIT: Compliant with OSHA's Lockout Standard designed to address risk and safety tagging in any facility
- We have confidence in our product. If you are not satisfied with our products, please contact us and we will reply to you within 24 hours.
8. Apply the relevant safety framework
OSHA’s Warehousing – Hazards and Solutions guidance covers conveyor inspection, guarding, jam response, and energy-control basics. OSHA’s Robotics – Overview notes that there are currently no OSHA standards written specifically for the robotics industry, but that does not eliminate other applicable workplace requirements or consensus standards. Applicability depends on the jurisdiction, equipment, employer, and integration.
ISO lists ISO 10218-1:2025, Edition 3, published in February 2025, for safety requirements for industrial robots as partly completed machinery. Integration into more complex systems is covered by ISO 10218-2. The catalog entry describes the scope of the standards; it is not a machine-specific troubleshooting procedure. Your risk assessment, local rules, and equipment documentation still determine how a particular cell must be serviced.
9. Prevent the next stoppage
After safe recovery, use the event to improve the installation rather than simply closing the alarm.
Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware matchWindows Errors? Fix Them Before They Spread
Repair common Windows errors and clear accumulated junk for a smoother, more stable PC - no reinstall needed.Free scan · no reinstall- Review the alarm history and the recorded sequence for recurring zones, products, shifts, or operating conditions.
- Inspect conveyors, guards, pinch points, sensors, tooling, cables, and transfer points on the schedule required by the equipment and site program.
- Check that operators know the boundaries of their permitted checks and the escalation contact for each zone.
- Keep current manufacturer manuals, electrical and pneumatic diagrams, recovery procedures, and lockout instructions at the point of use.
- Train authorized workers on the actual energy sources and verification steps for each robot cell and conveyor.
- Use controlled change management for recipes, software, network equipment, tooling, and product packaging so a recent change can be correlated with a stop.
- Review near misses, nuisance safety trips, and repeated jams even when production resumes; frequent resets can conceal a degrading safeguard or mechanical condition.
What not to assume
- A quiet motor means hazardous energy is gone.
- An emergency stop or protective stop explains why it activated.
- A robot alarm proves the robot is the failed component.
- A visible blockage can be removed safely by hand.
- A reset, power cycle, or homing command is safe on every installation.
- A lockout/tagout kit alone makes an untrained person qualified to service the equipment.
The safest first action is consistent across systems: protect people, preserve the exact fault information, inspect only what the procedure permits from a safe position, and escalate any guarded or energy-control work to authorized personnel.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

