
iTechGuides is reader-supported. When you buy through links on our site, we may earn an affiliate commission. As an Amazon Associate I earn from qualifying purchases. Learn more
Measure the surfaces that control fit—not every surface in the computer—then turn those measurements into a labeled sketch, a parametric model, and (when clearance is uncertain) a small test print. Record the opening, insertion depth, ledges, hole centers, retaining features, and nearby obstructions. A printed dimension copied exactly from the case can still fit badly because orientation, calibration, slicer settings, material, shrinkage, and warping all affect the result.
This workflow works for replacement brackets, covers, clips, cable guides, drive trays, fan adapters, and other custom parts. It does not provide model-specific case dimensions; those must be measured from your own hardware or obtained from an authoritative drawing for that exact model.
Start with the geometry that determines fit
Before opening a toolbox, decide how the new part interacts with the computer. A part may locate against a wall, slide into a channel, sit on a ledge, attach with screws, or flex over a clip. Those interfaces define the dimensions that matter.
Identify locating surfaces
Locating surfaces stop the part in a known position. For a case opening, measure its usable width and height, the depth available behind the opening, and the thickness of any lip or ledge that supports the part. For a replacement bracket, locate the faces that touch the chassis and the distance from those faces to the component being held.
#1 Best Overall
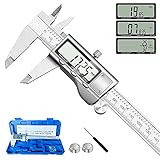
- 【STAINLESS STEEL MATERIAL】The vernier caliper is made of high-strength stainless steel and is waterproof and dirt-proof. The service life of this stainless steel digital caliper is longer than that of calipers with plastic or carbon fiber parts.
- 【ACCURATE MEASUREMENT AND ZERO SETTING】This digital caliper glides smoothly. Measuring range: 0 -6" / 0-150mm; Accuracy: ± 0.001"/ 0.02mm; Resolution: 0. 0005"/0. 01mm. At the same time, the smart design allows you to easily reset to zero by pressing a button and start a new measurement at any point on the scale, which is very suitable for differential measurement.
- 【4 MEASUREMENT MODES】The digital caliper has 4 measurement modes, which can be used to measure inside and outside diameter, depth, and step with two sets of jaws and a probe. Multiple measurement modes can bring more usage scenarios to people, and the measurement process is also very convenient.
- 【UNIT CONVERSION & LARGER LCD SCREEN】These Digital Calipers have a one-key button to quickly switch from inches (inch), fractions (F), millimeters (mm). The 6" digital caliper has a large, easy-to-read LCD DISPLAY which is easy to use and read even under strong sunlight. It will automatically turn off after 5 minutes of non-use to save power.
- 【Wide Applications】 Compared to the ordinary rulers, this stainless steel caliper can measure not only length but also caliber and depth, allows you to measure circular and cylindrical objects, more functions and better performance will satisfy you. It has always been used by professionals and hobbyists alike, jewelers, hobbyists, woodworkers, machinists, DIY, automotive mechanics, and more.
Identify retaining features
Retention may come from screw holes, slots, tabs, clips, magnets, or friction. Record hole diameter, center-to-center spacing, slot length and width, tab thickness, clip undercuts, and the direction in which the part is inserted. A hole’s diameter alone is not enough if its center is in the wrong location.
Map nearby clearance
Measure the nearest graphics card, radiator, fan, cable bundle, side panel, or other obstruction. Include the clearance needed for insertion and removal, not only the final installed position. A cover that technically fits when lowered vertically may fail if it must first slide past a component.
Measure movement ranges
If a screw, hinge, slider, or adjustable bracket moves, record the minimum and maximum available space. A replacement part may need to remain below a maximum thickness while still spanning a minimum gap. When a surface is hidden, derive its location from accessible reference measurements instead of guessing.
Do these 3 things before closing this tab:
1Repair Windows errors before they cause bigger problems2Fix the driver behind crashes, sound loss and screen glitches3Clear out junk files and repair common Windows errorsChoose tools that can actually reach the feature
A digital caliper is the primary tool for small openings, wall thicknesses, hole diameters, and depths. Check that it reads zero with the jaws closed, keep the jaws square to the surfaces, and repeat any reading where alignment is doubtful. Calipers, micrometers, and height gauges are manual inspection tools; use the one whose range and resolution suit the feature.
Use the right tool for each scale
- Digital caliper: external and internal dimensions, depths, step heights, and accessible hole diameters.
- Micrometer: repeatable measurements of small, accessible thicknesses when caliper resolution is not sufficient.
- Straightedge, ruler, tape, or square: long case dimensions that exceed the caliper’s span, and checks for alignment.
- Paper or card template: a curved or irregular outline that cannot be described by a few rectangular dimensions. Verify a template against direct measurements because tracing can shift or distort.
- Camera or phone notes: a visual record of which reference surfaces produced each number. A photograph is context, not a dimensional standard.
Do not force the instrument
Never wedge a caliper into a tight gap or use its jaws to pry a clip. For an obstructed dimension, measure from two accessible references and subtract one from the other when the geometry allows. If the part must remain installed while measuring, remove power and avoid contact with energized circuits.
Create a measurement plan before removing hardware
A short plan prevents the common mistake of collecting isolated numbers with no common datum. Select reference surfaces—the case floor, a panel edge, a mounting face, or a hole center—and measure every critical feature from those references.
Rank #2

- [INCH/MM Conversion]: One button can quickly convert two measuring unit (INCH/MM). Measuring Range:0 - 150mm (6") / Resolution: 0.01mm (0.0005")/Accuracy: ±0.02mm (0.001")
- [Stainless Steel Material]: The vernier caliper is made of high-strength stainless steel, which is waterproof, stain-proof and oil-proof. The ergonomic design brings you a comfortable feeling.
- [Large and Clear Display Screen]: Large LCD display gives you a clear reading. The thumb rolling and locking screw provide easy sliding, accurate positioning, and fine adjustment.
- [Multifunctional Use]: The digital micrometer can easily and accurately measure internal, external, height and depth dimensions.
- [Automatically shut off]: When you have no action on the dial caliper, it can automatically shut off after 4 minutes.
- Describe the function. Write whether the part locates, slides, presses, snaps, hinges, or simply covers an opening.
- Mark the datum. Choose the surface or centerline from which positions will be measured.
- List critical features. Include openings, depths, ledges, hole centers, slot ends, tabs, clips, and obstructions.
- Set units. Use millimetres consistently, and note the instrument and its displayed precision.
- Record ranges. For adjustable features, write minimum and maximum values rather than one average.
- Repeat questionable readings. Take a second reading after reseating the tool; investigate any difference instead of averaging blindly.
Measure the case and component step by step
1. Measure the opening
Measure the opening at more than one location if its walls may be tapered, rounded, or distorted. Record the smallest usable width and height when the printed part must pass through the opening. If a lip reduces the opening only on one side, note its position and thickness rather than treating the opening as a simple rectangle.
Free tools Windows power users keep installed
One-click scans. No signup required.
2. Measure insertion depth and ledges
Use the caliper depth rod or another suitable depth method to determine how far the part can enter. Measure the ledge that supports it and the distance from the ledge to the next obstruction. Distinguish between the maximum cavity depth and the depth available along the actual insertion path.
3. Locate holes and slots
Measure hole diameter and center-to-center distances from the same datum. For a slot, record overall length, width, end radius if relevant, and the location of its centerline. If a screw head or washer must sit flush, measure the counterbore or countersink as well.
4. Capture clips, tabs, and undercuts
Measure the tab’s width, thickness, and insertion length, plus the height and depth of the feature it hooks behind. Note the direction of flex and the space available for the tab to deflect. A rigid printed tab should not be modeled as though it were a metal spring without checking material behavior and wall thickness.
5. Check neighboring components
Measure clearance to the closest heat source, fan blade, connector, cable, or moving assembly. Include cable bend space and the room needed to unplug a connector. For a fan or radiator area, verify that the proposed part will not enter the sweep of moving blades or obstruct intended airflow.
PC Slower Than It Used to Be?
A free scan shows the junk files, broken settings and background clutter dragging Windows down - then fixes them in one click.Free scan · Windows 10 & 11Outdated Drivers Are Slowing You Down
One free scan finds every outdated or missing driver and matches the right update for your exact hardware.Free scan · exact hardware match6. Derive hidden dimensions
Suppose the distance from the case edge to a visible component is measurable, as is the distance from that edge to the far side of an obscured bracket. Subtract the two to obtain the hidden interval. Write the equation beside the result so a later change in either measurement can be propagated through the model.
Rank #3

- Best Cost-effectiveness: We've crafted this plastic digital caliper with a singular focus – delivering unmatched value at an unbeatable price. While others chase high-precision innovations, we prioritize essential features that truly matter.
- 4 Measurement Modes and Precision: Outside diameter, inside diameter, depth, and step measurements. Measurement range: 0-6 inches / 0-150 mm, accuracy: ±0.2 mm / 0.01 inches. Whether it's for home projects, DIY, or 3D print, having this caliper will elevate you to be a measurement star.
- Low Energy Consumption Design with Smart Auto-Off Function: With just a single battery, our caliper can support 8+ months of measurements. It can automatically turns on when you slide it, and turns off within 5 mins when not in use, effectively conserving battery power.
- Tough Plastic Case Packaging and Secure Measurements: The plastic case packaging effectively protects the caliper from external impacts and friction, ensuring that it stays in optimal condition at all times. Moreover, our digital caliper is made of extra strong carbon fiber composites that are not easy to damage the measured object during use.
- What You Get: Digital Caliper *1, Tough Plastic Case *1, and LR44 button batteries *3(with one pre-installed). Additionally, we offer a lifetime warranty and friendly customer service to ensure your complete satisfaction.
Make a labeled sketch that preserves context
A hand sketch is not a manufacturing drawing. Its purpose is to keep each number attached to the surface, hole, or edge it describes. Draw the part and its mating case feature in the same view when possible.
- Label every dimension with units.
- Use arrows that terminate on the actual measured faces.
- Mark the datum and the direction of insertion.
- Identify dimensions that are minimum, maximum, nominal, or derived.
- Circle measurements that still need confirmation.
- Annotate material thickness, screw head type, clip direction, and nearby obstructions.
For an irregular profile, make a paper template and add two or more known dimensions to it. Transfer the outline into CAD only after checking that those known dimensions scale correctly. A shifted trace can otherwise produce a part that looks right but is uniformly the wrong size.
Build the model around constraints, not guesses
In CAD, create a dimensioned sketch or parametric model from the measured interfaces. Constrain the surfaces that must touch, the faces that must slide, and the centers that control attachment. Keep nominal measurements separate from fit allowances so you can change tolerance without redrawing the part.
Quick wins for a faster PC:
Scan for outdated or missing drivers - takes under a minuteDriver Scan →Repair Windows errors before they cause bigger problemsFix Now →Separate functional geometry from clearance
Model the case-facing opening, hole pattern, or locating shoulder from the measured nominal geometry. Then add explicit clearance to the mating feature. This makes the reason for each offset visible and allows a printer-specific adjustment later.
Inspect critical dimensions in CAD
Use the CAD inspection tools to check feature diameters, distances between parallel faces, and center-to-center distances. Compare the measured values with the model’s nominal dimensions and any tolerances you have recorded. Also inspect wall thickness, sharp internal corners, and interference between the new part and neighboring geometry.
Check printer-related requirements
Measure the modeled feature in CAD before exporting. Confirm that holes, thin walls, bridges, overhangs, and clearances are appropriate for the printer and process you intend to use. A design can be dimensionally correct yet difficult to print or too fragile in its chosen orientation.
Rank #4
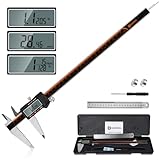
- 【Stainless steel material】Digital calipers are made of high quality stainless steel, waterproof and rustproof, and the sturdy frame reduces the wear and tear of vernier calipers, allowing a longer service life
- 【Accurate measuring range】 0-12 inches/300mm; Display: 14mm x 40mm oversized LCD; Accuracy: ±0.04mm/0.0015 inches; Resolution: 0.01 mm/0.0005 inches. The knurled thumb roller ensures smooth gliding in use; the locking screw enables accurate positioning. These two designs ensure smooth operation during measurement and prevent slippage or jams from occurring
- 【4 measurement modes】The digital caliper comes with two pairs of jaws and a probe to easily measure depth, step length, outside diameter and inside diameter. Four measurement methods meet most of your measurement needs
- 【3 unit conversions】 With the push of a button, you can quickly switch between the 3 units of the digital caliper: inches, millimeters and fraction; plus the large LCD screen makes it easy to read. You can reset it to zero with the zero button, plus the digital vernier caliper will automatically turn off after 5 minutes of non-use to save power
- 【Wide application】HARDELL digital caliper comes with 1*ruler, 1*screwdriver, 2*batteries. The case is resistant to pressure, shock and drop for easy storage and carrying. 12 inch caliper micrometer has been used by professionals and amateurs, it is the best choice for mechanics, woodworkers, jewelers, craftsmen, DIY enthusiasts, auto mechanics, etc
Understand why exact measurements still need tolerance
A physical case dimension is not a guaranteed printed dimension. Printed parts can shrink or warp, and the result changes with model size, orientation, interlocking geometry, calibration, layer settings, and material. Prusa Research states: “When modeling parts that should fit together, you need to include a certain amount of tolerance.”
Recommended Free Tools
Prusa’s guidance gives at least 0.2 mm as a stated accuracy for an Original Prusa printer and at least 0.3 mm as an initial measurement for movable parts. These are manufacturer guidance figures for that printer context, not universal clearance rules or performance statistics. Treat them as starting points only, then adjust from an actual test print.
Choose tolerance by function
| Fit function | What to measure | Design decision | Risk to check |
|---|---|---|---|
| Locating fit | Reference faces, opening size, insertion depth | Allow enough clearance to seat without binding while preserving repeatable location | Warped edges or debris can prevent seating |
| Sliding fit | Full travel, parallel faces, end stops | Provide clearance along the entire travel path, not just at the entrance | Layer seams, elephant’s foot, and material friction can cause binding |
| Press fit | Actual mating diameters and insertion force available | Use a controlled interference only after a coupon test | Excess force can crack the print or damage the case |
| Snap fit | Undercut, flex length, deflection space, retention force | Provide room for the arm to flex and avoid sharp stress risers | Repeated flexing and heat may reduce retention |
| Cover or guard | Perimeter, supports, fasteners, nearby moving or hot parts | Prioritize non-contact clearance and service access | Interference can block cooling or maintenance |
Use a small fit-test print before the full part
When a clearance or hole pattern is uncertain, print only the critical feature: a short section containing the opening, tab, screw hole, or sliding channel. Test it in the real case using the same printer, material, layer settings, orientation, and build-surface conditions planned for the final part.
- Copy the measured interface into a simple test coupon.
- Include several nearby clearance values or interchangeable inserts if the design is still uncertain.
- Print the coupon with the orientation and settings intended for the final part.
- Remove first-layer artifacts before judging the fit.
- Test insertion, removal, retention, and movement—not just whether the pieces can be forced together.
- Record the observed adjustment and apply it parametrically to the final model.
Autodesk notes that printing materials can shrink or warp and recommends comparing a printed test part with nominal dimensions. A test coupon is cheaper and faster to revise than a complete bracket or panel, and it exposes printer-specific behavior before the final print consumes more material.
Independent reader supportYour contribution helps us test, update, and keep practical guides available for everyone.Use slicer measurement tools correctly
A slicer can help inspect an existing model. PrusaSlicer’s Measurement tool checks dimensions and angles on a single object, which is useful for confirming a hole, wall, or angle in the file. It is not a substitute for measuring the physical case.
What’s actually slowing this PC down?
Pick the symptom - the matching free tool is one click away.
The documented tool has limitations: it does not measure between separate objects, and overlapping parts and negative volumes can produce imperfect results. For comparisons between the case and a new part, use physical measurements and CAD assembly or interference checks rather than relying on a slicer overlay.
Best Value

- Solid stainless steel build – This digital caliper 6 inch resists rust, wear, and corrosion, outlasting plastic models. The sturdy metal body handles daily workshop use without bending. The shockproof case protects your measuring tool from drops and impacts, keeping it safe and ready for each job
- Reliable accuracy with smooth glide – This digital vernier caliper measures 0‑6″ / 0‑150mm with ±0.02mm / 0.001″ accuracy and 0.01mm resolution. The thumb roller glides without sticking, and the locking screw holds your reading steady. From checking 3D print filament and woodworking joints to measuring jewelry and small parts for repairs, you can trust the results
- Four measurement modes in one – Use two jaw pairs and a depth probe for ID, OD, depth, and step measurements. No need to switch digital caliper measuring tool – this versatile dial caliper covers tubing, bores, recesses, and shoulders. Press the zero button anywhere to reset for quick comparative checks. Close and re‑zero before each use to ensure consistent readings
- Metric & Imperial conversion with large LCD – This electronic vernier caliper lets you switch between millimeters and inches with one click. The oversized LCD screen displays crisp, bold numbers that are easy to read at a glance. The wide viewing angle means you can read it clearly without tilting the caliper. Auto‑off powers down after 5 minutes of non‑use to save battery
- Complete kit – ready out of the box – Your package includes the digital micrometer, a sturdy case, two batteries (one spare), a mini screwdriver, and a stainless steel ruler. No extra trips to the store – just open and start working. A practical choice for DIYers, hobbyists, and makers who need reliable measurements at home or in the workshop
Troubleshoot a part that does not fit
The part is too tight everywhere
Check first for a zeroing or unit error, then measure the printed feature at several points. Look for first-layer expansion, warping, or an orientation-dependent dimension change. If the printer is consistently oversized, adjust the model or process based on a calibration result; do not remove material from a critical case feature without confirming the cause.
Only one corner binds
Inspect the case for taper, a burr, or a twisted printed base. Recheck diagonal dimensions and the squareness of the mating surfaces. A single global clearance change may hide the actual problem; revise the local constraint or correct the print’s warping.
Screw holes do not align
Re-measure center-to-center distances from one datum rather than measuring each hole from a different edge. Confirm whether the original fastener uses a countersink, counterbore, shoulder, or washer. A hole diameter can be correct while the pattern is misplaced.
A snap tab breaks
Check insertion direction, available deflection space, layer orientation, wall thickness, and sharp internal corners. Reduce required deflection or redesign the retention feature rather than simply increasing interference. If the part is exposed to heat, validate the material and geometry for that environment; the general fit guidance does not certify a structural or heat-critical application.
The part fits cold but interferes after assembly
Measure with cables, panels, and adjacent components installed as they will be in use. Check movement envelopes for fans, hinges, and sliding panels. Include service and cable-routing clearance in the model, not only the static gap measured on an empty case.
Final measurement and print checklist
- Function, insertion direction, and datum are written down.
- Opening width and height, depth, ledges, and nearby clearances are recorded.
- Hole or slot centers, diameters, head recesses, clips, and tabs are dimensioned.
- Minimum and maximum positions are captured for moving features.
- Caliper zero and jaw alignment were checked; long dimensions were measured with a suitable tool.
- Derived dimensions include the subtraction or construction used to obtain them.
- A labeled sketch links every critical number to a physical surface.
- CAD constraints distinguish nominal geometry from printable clearance.
- Printer orientation, material, settings, shrinkage, and warping are considered.
- A small test coupon is planned for any uncertain fit.
- The assembled part will not obstruct airflow, moving components, connectors, or service access.
What a reliable measurement process can—and cannot—promise
Careful interface measurements, a common datum, explicit CAD constraints, and a fit-test print greatly reduce failed iterations. They cannot produce one clearance value that works on every printer, material, orientation, or geometry. Treat the figures published for a particular printer as starting guidance, validate the critical feature on your own setup, and preserve the measured context so the design remains editable when the case or print process changes.
Quick Recap
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon at the time of purchase will apply.

